Pharmaceutical & Medical-Grade Floors​

Epoxy Flooring & More For Your Pharmaceutical & Medical Spaces

Did you know?

Spaces that require unique flooring solutions include: Chemical Storage Rooms, Corridors, ISO/Clean Rooms, Laboratories, Restrooms and Locker Rooms, Shower Rooms, Sterile Areas, Vivariums, Wash Rooms, and Wash Bays.

01

Leave "Ground-Breaking" to Your Research

While you breach the edges of innovation and progress, we’ll provide the precise science required for ergonomic, highly sanitary floors that are also chemical-resistant. AppliedeX can provide your facility with the highest-performance chemical, impact, water, and abrasion-resistant, seamless flooring systems that specifically serve the pharmaceutical, medical, biotechnology, health research, and healthcare industries.

02

Why Your Pharmaceutical & Medical Spaces Need Our Solutions

Our flooring solutions include pharmaceutical flooring, pharmacy flooring, and medical grade flooring, such as epoxy flooring for the pharmaceutical industry and bacteriostatic flooring.

Hygienic Compliance

Specialized flooring solutions help maintain strict cleanliness and hygiene standards essential in pharmaceutical environments.

Antimicrobial Properties

Flooring systems with antimicrobial treatments inhibit the growth of bacteria and other pathogens, ensuring a safer environment.

Static Control

Static dissipative flooring helps prevent electrostatic discharge, protecting sensitive electronic equipment and products.

Chemical Resistance

Our flooring solutions withstand spills from harsh chemicals and solvents commonly used in pharmaceutical manufacturing.

Temperature Stability

Certain flooring systems help manage temperature variations, crucial for sensitive products.

Regulatory Compliance

Our solutions are designed to meet industry regulations and standards, ensuring that facilities operate within legal requirements.

03

Benefits Of Our Solutions

These flooring systems are designed to meet the stringent hygiene and contamination control standards required in pharma manufacturing, medical laboratories, hospitals, and biotech facilities.

Seamless Design

Seamless flooring prevents dirt and contaminants from accumulating in seams, making cleaning more efficient.

Durability

High-quality materials ensure long-lasting performance, reducing the need for frequent replacements or repairs.

Easy Maintenance

Flooring solutions are designed for easy cleaning, facilitating compliance with regulatory requirements.

Customization

Tailored flooring options can be designed to meet specific operational needs and regulatory guidelines.

05

Trust Us With Your Medical-Grade Flooring

Our hygienic flooring for pharma labs and healthcare facilities is thermal shock resistant, slip resistant, and easy to clean, ensuring compliance with cleaning protocols and maintaining hygiene. Additionally, our epoxy flooring pharmaceutical solutions are stain resistant and chemical resistant, making them ideal for research facilities and other critical environments.

Contact us today to learn more about how our medical and pharmaceutical flooring services can benefit your project.

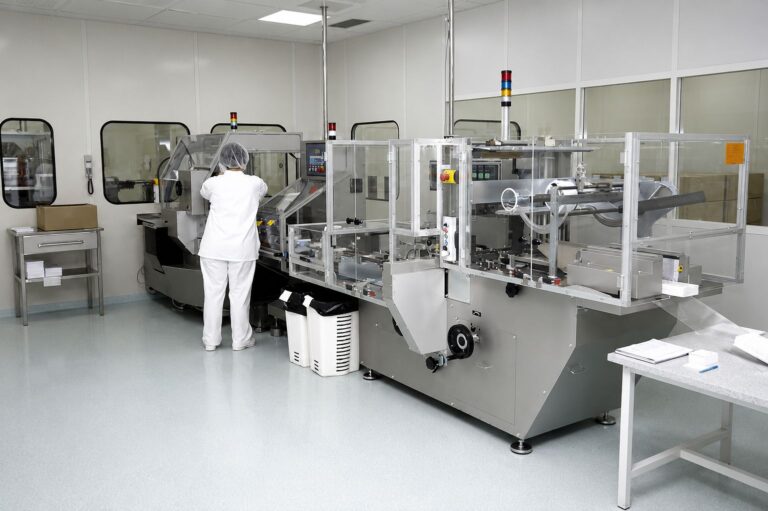
Cleanroom manufacturing facility, automated machinery, light blue industrial flooring.
06

Our Services

AppliedeX provides a full suite of specialized flooring services for pharmaceutical and medical manufacturing, including surface preparation, precision slab correction, cove installation, and hygienic coating application to ensure compliance and contamination‑control.

  • Pharmaceutical Flooring Installation
  • Clean Room Flooring Solutions
  • Antimicrobial Flooring Systems
  • Seamless Flooring Installation
  • Surface Preparation and Repair
  • Customizable Flooring Options
  • Chemical Resistance Flooring
  • Static Control Flooring
  • Maintenance and Cleaning Services
  • Consultation and Compliance Services
07

Our Systems

AppliedeX provides a full suite of GMP‑focused flooring systems engineered for pharmaceutical, biotech, and medical manufacturing environments, delivering seamless, hygienic, and contamination‑resistant surfaces that support strict regulatory compliance and cleanroom performance.

  • Epoxy Flooring
  • Polyurethane Flooring
  • Seamless Resin Flooring
  • Epoxy Quartz Flooring
  • Antimicrobial Coatings
  • Static Dissipative Flooring
  • Durable Epoxy for Hallways
  • Clean Room Flooring Solutions
  • Moisture Mitigation Systems
  • Chemical Resistant Flooring
Surgical suite industrial flooring, stainless steel worktops, medical lights, cabinets.
08

Frequently Asked Questions

Pharmaceutical floors use seamless, non‑porous resin systems that eliminate joints, gaps, and micro‑harborage points where bacteria can grow. Their smooth, chemical‑resistant surfaces allow for frequent sanitization and meet strict cleanroom hygiene requirements.

High‑performance epoxy, urethane, and ESD‑rated coatings are engineered to withstand aggressive disinfectants, biofluids, alcohols, and cleaning agents used in GMP environments. These systems maintain integrity under constant washdowns and sterilization cycles.

Pharma‑grade floors are designed to meet FDA, GMP, ISO cleanroom, and USP standards. They provide traceability, durability, and hygiene performance that align with regulatory expectations for contamination control and quality assurance.

AppliedeX delivers contamination‑controlled flooring engineered for the precision, sterility, and compliance demands of pharmaceutical manufacturing, cleanrooms, labs, and medical facilities. Our systems are built to support GMP workflows, withstand harsh disinfectants, and maintain long‑term hygiene performance.

  • Cleanroom‑Ready, Seamless Installations AppliedeX floors eliminate cracks, grout lines, and joints, creating a fully hygienic surface ideal for sterile environments.

  • Engineered For Chemical And Disinfectant Resistance Our resin systems are formulated to endure repeated exposure to alcohols, peroxides, sanitizers, and biohazard cleanup protocols.

  • GMP‑Aligned Design And Documentation We provide installation methods, QA processes, and traceability that support audits and regulatory compliance.

  • ESD And Specialty Performance Options For labs, compounding areas, and device manufacturing, we offer ESD‑rated, antimicrobial, and high‑durability systems tailored to each space.

  • End‑To‑End Expertise From surface prep to installation to long‑term maintenance, AppliedeX ensures consistent, validated performance across your facility.

Contact the Pharmaceutical & Medical-Grade Flooring Experts

Trust AppliedeX for stringent hygiene and contamination control standard flooring requirements

Call or contact us today and request a quote to transform your space with our solutions.

How Ready Is Your Floor For Automation?