Food & Beverage Processing, Commercial Kitchen Flooring

Seamless CFIA, USDA, FDA and OSHA-Approved Epoxy Flooring for the Food and Restaurant Industries

Did you know?

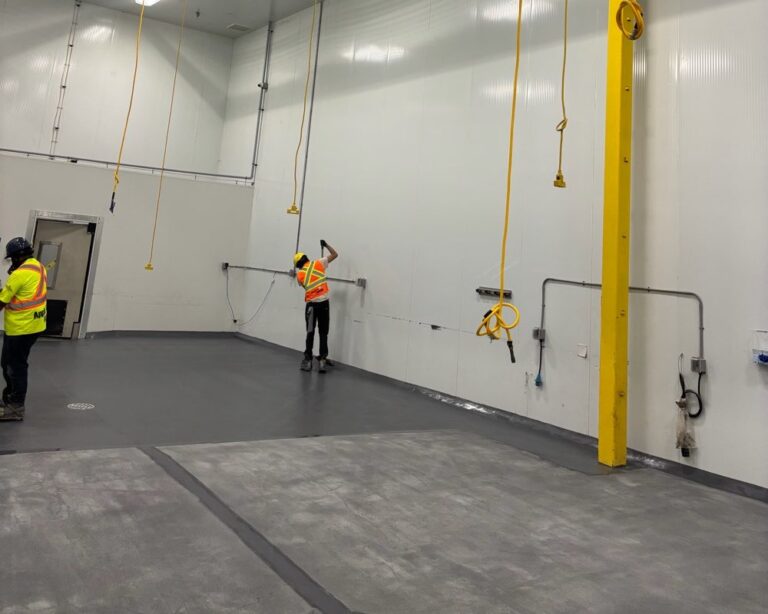
We install USDA, OSHA, and FDA-approved resinous flooring, designed to handle temperature shocks from 5°C to 100°C. These systems are commonly used in institutional kitchens, high-end restaurants, food manufacturing plants, and breweries.

01

Clean Enough To Believe In The 5 Second Rule

Food and beverage facilities—including grocery stores, food processing plants, warehouses, commercial kitchens, breweries, wineries, distilleries, and pet food production lines—have unique and demanding flooring requirements. Floors must withstand extreme temperatures, moisture, chemical sanitization, washdowns, and heavy traffic, while remaining compliant with CFIA, USDA, FDA, OSHA, SFCR, and FSMA standards. At AppliedeX, we specialize in seamless, sanitary, and durable flooring systems designed to meet these stringent demands across all sectors.

02

Why Your Food & Beverage Plants or Restaurants Need Our Solutions

From major clients like Molson and Pepsi Bottling Group to small commercial kitchens, AppliedeX provides tailored flooring for packaging plants, coolers, fryer lines, restrooms, wash bays, and more. Whether aesthetics or function is the priority, our flooring stands up to every challenge in the food and beverage industry.

Safety Assurance

Our flooring solutions are designed with safety in mind, incorporating anti-slip, microbial and chemical properties to protect both personnel and equipment.

Chemical Resistance

Specialized coatings protect against harsh chemical wash downs, ensuring a safe and clean working environment each and every day.

Moisture Control

Our flooring systems include moisture barrier solutions that protect against water damage and help maintain optimal conditions for food and temperature-safe storage.

Thermal Protection

Seamless flooring prevents contaminants from accumulating in seams, facilitating easier cleaning and enhancing overall hygiene.

Seamless Design

Specialized coatings protect against harsh chemical wash downs, ensuring a safe and clean working environment each and every day.

03

Benefits Of Our Solutions

With a strong track record in the food and beverage sector, AppliedeX is a trusted partner for flooring solutions that enhance productivity and safety.

Value Engineering

Our solutions are optimized for cost-effectiveness, providing long-term savings through reduced maintenance and replacement costs.

Customization

Tailored flooring options can be designed to meet specific operational needs, maximizing functionality in food and beverage production facilities.

Quick Installation

Our experienced team ensures efficient installation, minimizing downtime and keeping production on track.

04

Food and Beverage Flooring Clients We've Served

05

Trust Us With Your Food & Beverage Plants Or Commercial Restaurant Floors

AppliedeX’s food and beverage flooring solutions are ideal for Packaging Plants, Commercial Kitchens, Brewing, Bottling and Bagging Areas, Bakeries, Freezers and Refrigeration, Loading Docks, Aisleways, Battery Charging Areas, Cafeterias, CIP Areas, Coolers and Freezers, Soup Kettles, Fryer Lines, Intake Areas, Loading Docks, Production and Processing Areas, Restrooms and Locker Rooms, Stairwells, Warehouses, Wash Rooms and Wash Bays.

Contact us today to learn more about how our Food and Beverage Manufacturing or Industrial Restaurant flooring services can benefit your project. 

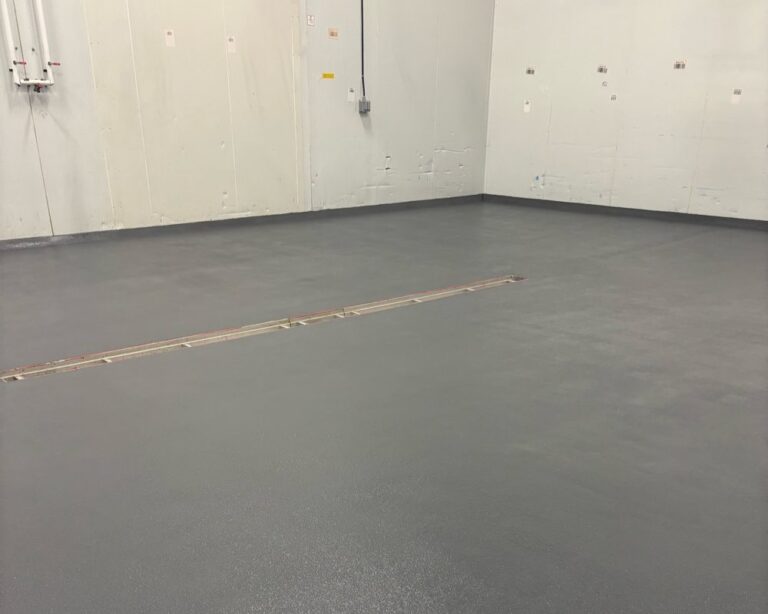
Durable blue industrial epoxy flooring, machinery, pipes, integrated floor drains.
06

Our Services

We provide tailored flooring services for packaging plants, coolers, fryer lines, restrooms, wash bays, and more.

  • Specialized Flooring Installation
  • Seamless Flooring Systems
  • Advanced Drainage Solutions
    Surface Preparation and Repair
  • Moisture Control Solutions
  • High Impact Resistant Coatings
  • Durable and Heavy-Duty Flooring
  • Anti-slip Treatments
  • Maintenance and Cleaning Services
  • Consultation on Regulatory Compliance
07

Our Systems

AppliedeX supplies a complete set of food safe floor systems.

  • Anti-Microbial Epoxy Flooring
  • Thermal Shock/Cycling Resistant Flooring
  • Polyurethane Flooring
  • Seamless Resin Flooring
  • Abrasion Resistant Flooring
  • Chemical Resistant Coatings
  • Heavy-duty Concrete Coatings
  • Moisture Barrier Systems
  • Anti-slip Flooring Systems
  • Thermal Insulating Flooring
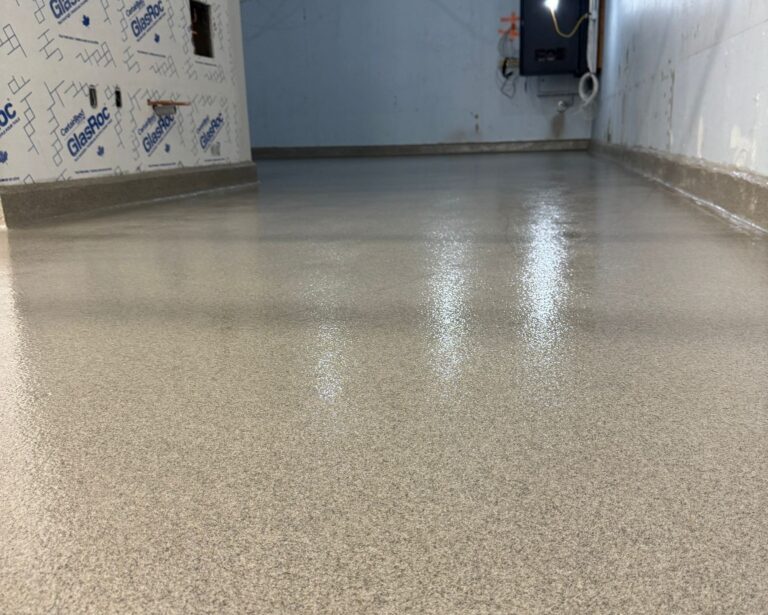
AppliedeX industrial seamless flake flooring, durable, integrated cove base.
08

Frequently Asked Questions

Food safe epoxy is one of the most installed industrial flooring systems that AppliedeX installs. With some of North America’s largest food and beverage manufacturers choosing Applied to install their food-grade floors, food, beverage, brewery and pet food manufacturing floors are truly our specialty. 

Thermal cycling is the rotation of hot, cold and consistently varying temperatures that occur typically in food and beverage production facilities. Floors are exposed consistently to these types of extreme conditions due to processing steps, equipment output, and regular cleaning and hot-water washdowns. It is imperative that food and beverage processing floors withstand this constant stressful cycling in order to prevent cracking of the floor, keeping them seamless,  antibacterial (FDA & CFIA compliant), durable and safe for employees.
In breweries, wineries, and distilleries, floors must resist damage from alcohol, yeast, and spills. Heavy-duty urethane systems offer the heat, chemical, and water resistance needed in brewing, kegging, canning, and bottling areas, while epoxy systems serve restaurant spaces with skid-resistant, easy-to-clean surfaces.
Pet food processing facilities, regulated by SFCR and FSMA, require similar sanitary and seamless flooring. Whether producing wet or dry pet food, we customize flooring solutions to ensure compliance and safety. Sloping, drainage, and epoxy curbs may also be necessary for washdown zones.

We bring decades of expertise to deliver leading food and beverage processing to fit your needs. Here’s why businesses with packaging plants and kitchens trust us:

  • Expertise in Food & Beverage Safe Applications: AppliedeX has specialized knowledge in flooring systems designed for the unique needs of food and beverage environments, ensuring stringent cleanliness & optimal performance.

  • Resistance to Spills: Our flooring solutions are highly resistant to various spills, including chemicals and electrolytes, which are critical for maintaining safety and functionality.

  • Durable Materials: We use high-quality materials that withstand the demanding conditions of food production and storage, ensuring longevity and reliability.

  • Customized Solutions: AppliedeX offers tailored flooring options that address specific operational requirements, providing maximum efficiency and safety.

  • Seamless Installation: Our seamless flooring prevents contaminants from accumulating, making cleaning easier and enhancing overall hygiene.

  • Sanitary and Employee Safety Focus: We prioritize safety by ensuring our flooring solutions meet stringent safety standards, protecting both workers and equipment.

  • Efficient Installation: Our experienced team ensures quick and effective installation, minimizing disruption to production schedules.

  • Comprehensive Support: Beyond installation, we provide ongoing maintenance and support to keep flooring in optimal condition throughout its lifecycle.

  • Proven Track Record: AppliedeX has successfully completed projects in the food & beverage manufacturing and industrial kitchen sectors, establishing a reputation for reliability and quality.

  • Commitment to Customer Satisfaction: We work closely with clients to understand their needs and deliver solutions that exceed expectations, ensuring a positive experience from start to finish.

Contact the Food & Beverage Handling Facilities Experts

Trust AppliedeX for all your food safe flooring needs.

Call or contact us today and request a quote to transform your space with food and beverage flooring solutions.

How Ready Is Your Floor For Automation?